How Conveyor Systems Improve Efficiency in Modern Warehousing
In the ever-evolving landscape of modern warehousing, operational efficiency has become paramount. As businesses strive to meet the ever-increasing demands of consumers, the integration of advanced technologies in their logistics frameworks has proven essential. Among these technologies, conveyor systems stand out as a crucial component that greatly enhances organisational efficiency, productivity, and accuracy in material handling.
The utilisation of conveyor systems in warehousing offers a multitude of advantages, ensuring that goods are moved swiftly and safely throughout the supply chain. From the transportation of raw materials to the distribution of finished products, conveyors facilitate a seamless flow of operations that reduces manual handling, lowers operational costs, and optimises space. This article delves into the various ways in which conveyor systems contribute to efficiency in contemporary warehouses while exploring their different types and applications.
Streamlining Material Handling
One of the primary benefits of conveyor systems is their ability to streamline material handling processes. Traditional warehousing often relies heavily on manual labour for the movement of goods, which can be not only time-consuming but also prone to human error. By incorporating conveyor systems, organisations can automate the movement of products, thereby minimising the risk of misplacement or damage.
Conveyor systems accelerate the transportation of items across various warehouse areas, facilitating rapid loading and unloading of goods. This automation helps in significantly reducing the time taken to fulfil orders and expedites the entire supply chain process. Moreover, with conveyors working continuously, warehouses can handle larger volumes of inventory efficiently, ensuring that organisations can keep pace with rising consumer demands and avoid stock shortages.
Reducing Labour Costs
In an era where reducing overheads is critical for competitiveness, conveyor systems offer substantial savings on labour costs. With the automation of material movement, businesses can limit the number of employees needed for manual handling tasks. This not only results in lower labour expenses but also enables staff to focus on more value-added activities, such as quality control and inventory management.
While the initial investment in conveyor systems may seem significant, the long-term savings often justify the expenditure. By minimising labour costs, organisations can allocate their resources more efficiently, thereby enhancing overall profitability. Additionally, automated systems can operate around the clock, ensuring that warehouses run at maximum productivity without the limitations imposed by shift patterns and employee availability.
Optimising Space Utilisation
Warehouse space is a precious commodity that can significantly impact operational costs. Effective utilisation of available space is vital in enhancing warehouse efficiency, and conveyor systems play a key role in this area. Unlike traditional methods of storing goods, which often require expansive floor space for manual handling, conveyor systems can be designed to maximise vertical space and optimise layouts.
Modern conveyor systems come in various configurations, from horizontal and vertical conveyors to automated storage and retrieval systems (AS/RS). This flexibility allows warehouses to adjust their operations to fit their spatial constraints. For example, inclined conveyors can transport goods to upper levels without requiring extensive ground-level space, while modular conveyor systems can be tailored to specific warehouse designs, promoting optimal space utilisation.
Enhancing Accuracy and Inventory Management
Another significant advantage of conveyor systems is their ability to improve accuracy in inventory management. Manual handling is often subject to human error, leading to misplaced items and discrepancies in stock levels. Conveyor systems, equipped with advanced tracking technologies and sensors, enable real-time monitoring and precise control of inventory as it moves through the warehouse.
With integrated systems capable of scanning barcodes or RFID tags, organisations can maintain precise records of their inventory levels, ensuring that stock data is consistently updated. This accuracy not only aids in efficient stock replenishment but also enhances visibility into the supply chain, allowing businesses to make informed decisions about their inventory management strategies.
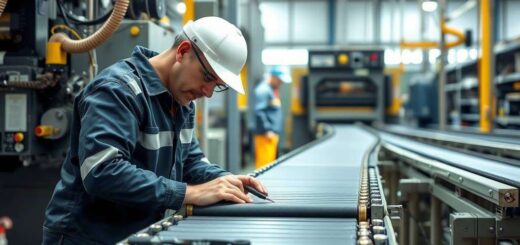
Conveyor systems are essential for streamlining production and logistics processes in various industries. By optimizing material handling, these systems improve efficiency and reduce labor costs. Explore the latest innovations in conveyor systems to enhance your operations and meet evolving demands in today’s fast-paced market.
Facilitating Flexibility and Scalability
The dynamic nature of modern businesses demands flexibility and scalability in warehousing operations. Conveyor systems provide the adaptability required to respond to fluctuating market demands. As businesses grow, their warehousing needs often change, necessitating a system capable of accommodating new products and processes.
Modular conveyor systems can be easily reconfigured or expanded without significant disruption to existing operations. This agility enables organisations to pivot quickly in response to market changes, ensuring they remain competitive in their industry. Whether it entails adding new conveyor segments or incorporating advanced technologies such as robotics, conveyor systems can evolve alongside a business’s needs.
Conclusion and Future Outlook
As we witness the transformation of warehousing into a highly automated and technology-driven sector, conveyor systems remain a linchpin in optimising operational efficiency. Their ability to streamline material handling, reduce labour costs, optimise space, enhance accuracy, and provide flexibility positions them as an indispensable asset in modern logistics. As technology continues to advance, the integration of conveyor systems is likely to become even more sophisticated, further driving efficiencies and reshaping the future of warehousing.